Solutions
Built Around Your Process, Not a Catalogue
Six industries, six different sets of constraints. Pick yours and see how we approach it.
Industry
Meat & Slaughtering
From live receiving through chilling, maturation, segmentation and blast freezing to finished-goods storage.
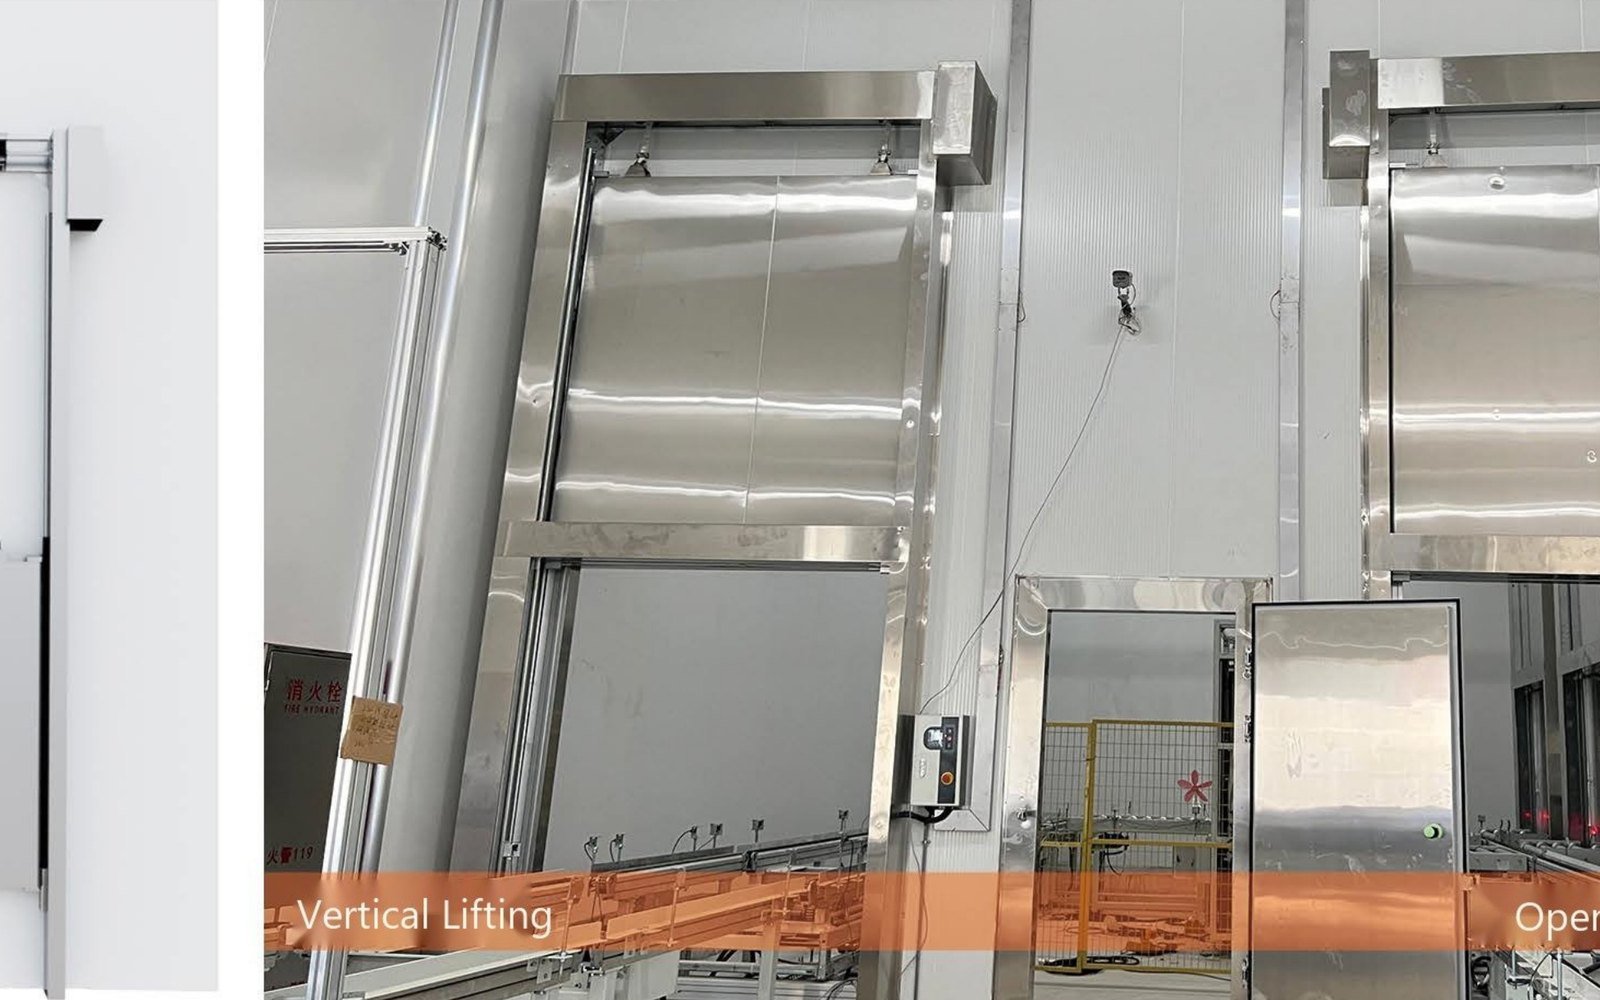
Meat plants need several temperature regimes inside one building — and the transitions between them are where quality is lost. We design the chilling and maturation rooms, the blast freezers and the cold store as one continuous system, so product moves on the correct temperature curve from carcass to carton.
Industry
Seafood & Aquatic
Rapid chilling and IQF freezing that protects texture, yield and shelf life.
Seafood loses value fast. The gap between catching and reaching −18 °C core determines drip loss, texture and shelf life. Our IQF spiral and fluidised-bed freezers are sized for the shortest practical freezing time, and the pre-chilling stage is designed to remove the bulk of the heat before the freezer.
Industry
Fruits & Vegetables
Pre-cooling, cold storage and IQF lines for fresh and processed produce.
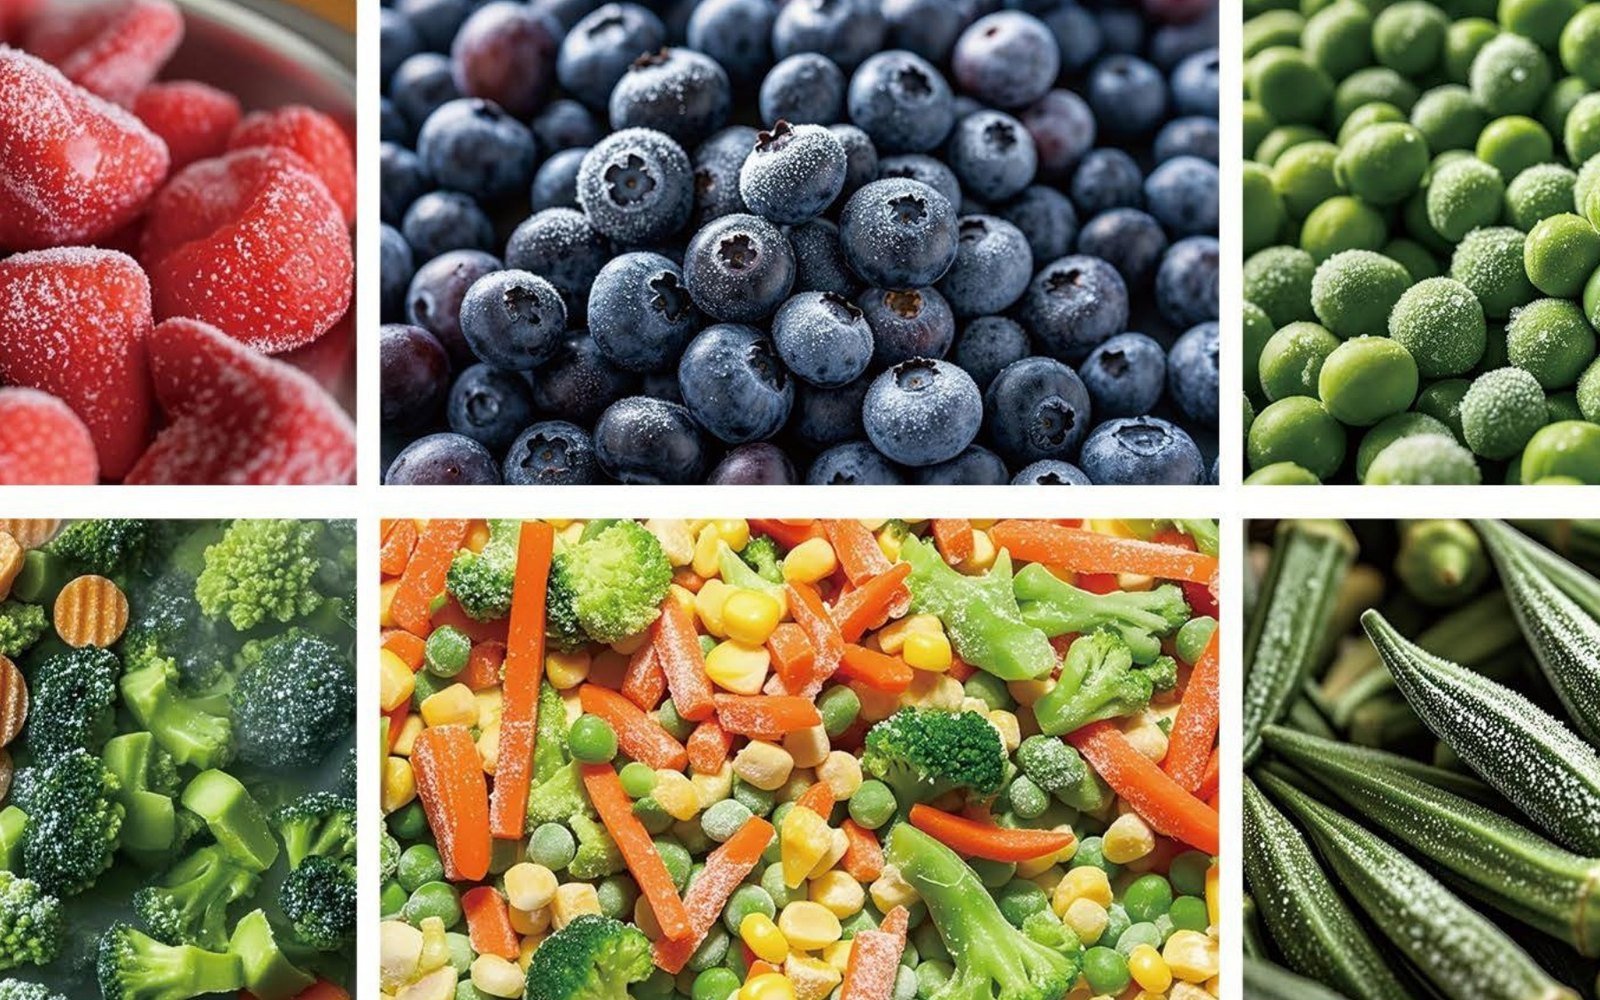
Produce is alive after harvest — it respires, and respiration is what ages it. Pre-cooling immediately after harvest, followed by correctly humidified cold storage, is what buys shelf life. We design vacuum and forced-air pre-cooling, high-humidity rooms and IQF lines for processed product.
Industry
Prepared & Convenience Food
Spiral freezing and hygienic process rooms for ready meals and bakery.
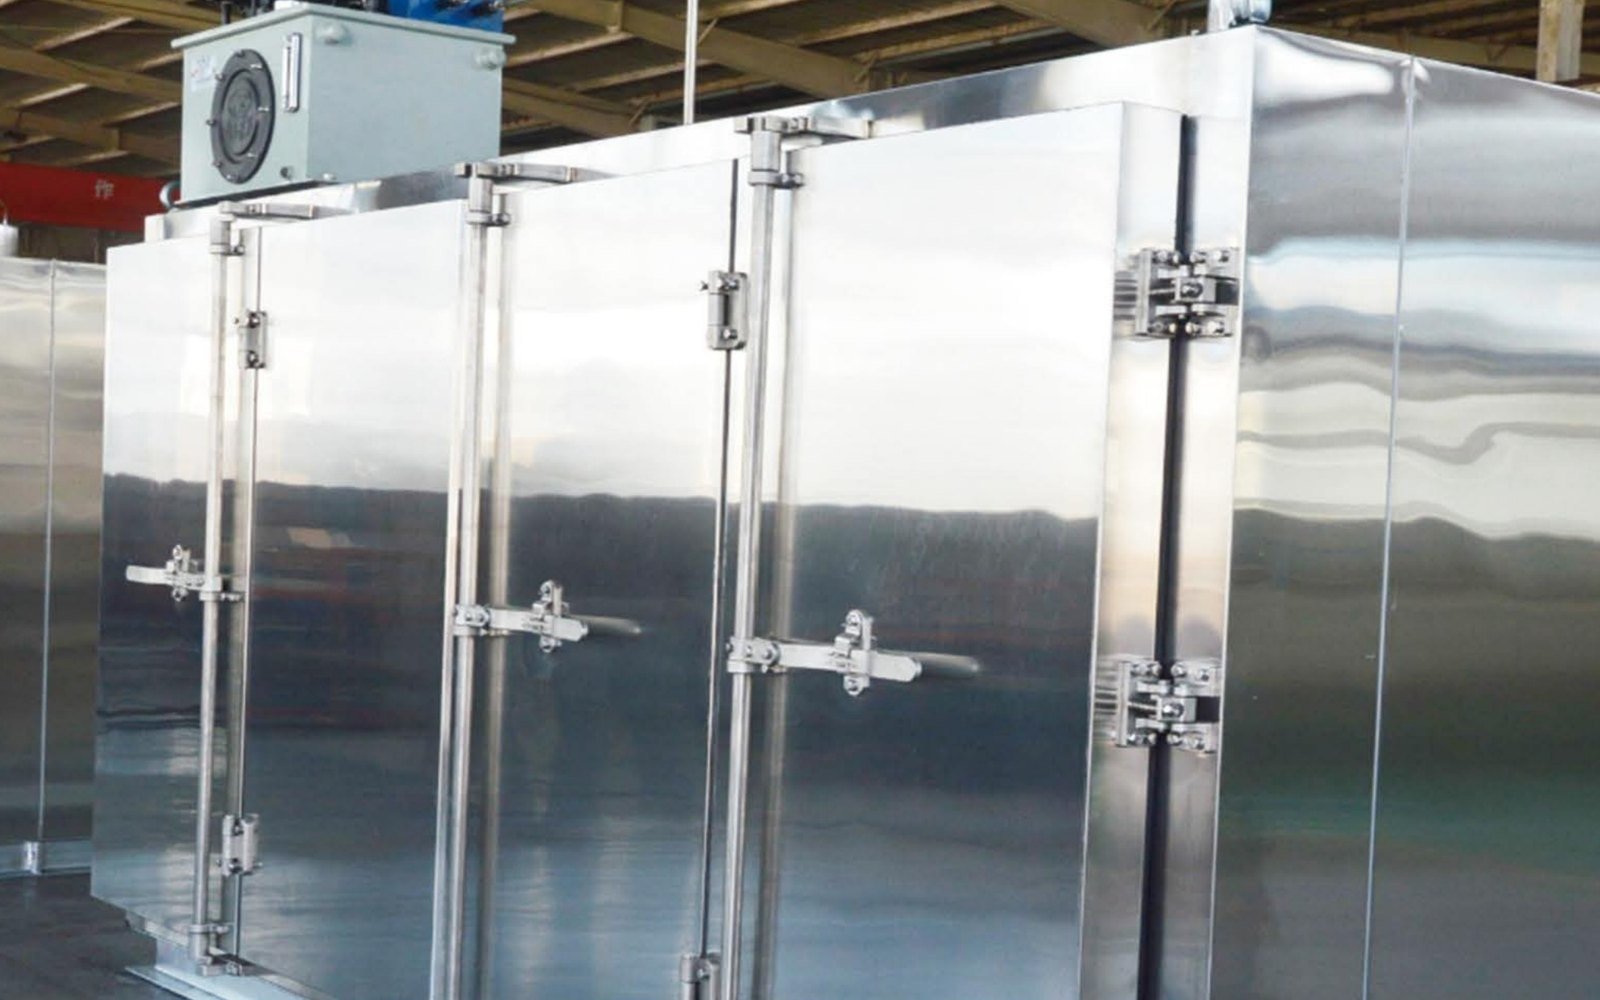
Ready meals and bakery products are frozen in packaging, at high line rates, in rooms that must be cleanable to food-safety standards. We combine hygienic panel systems, washdown-tolerant doors and spiral freezers sized to the line rate, with controls that record the freezing curve for your HACCP documentation.
Industry
Cold Chain Logistics
Distribution centres, loading docks and multi-temperature storage.
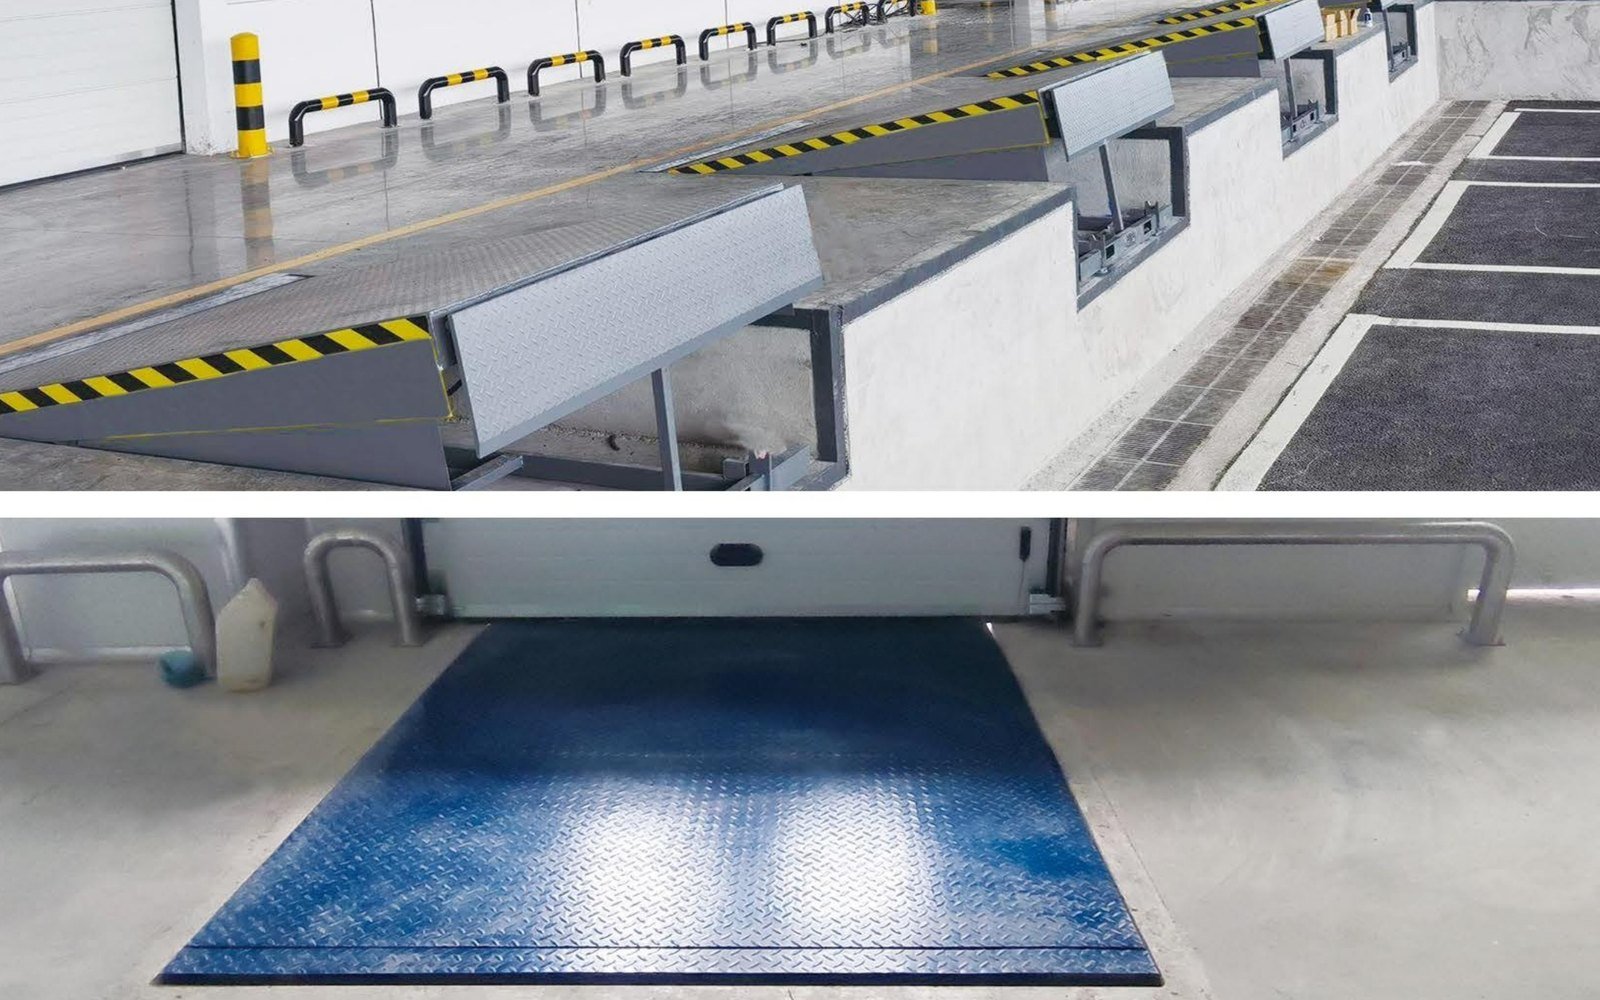
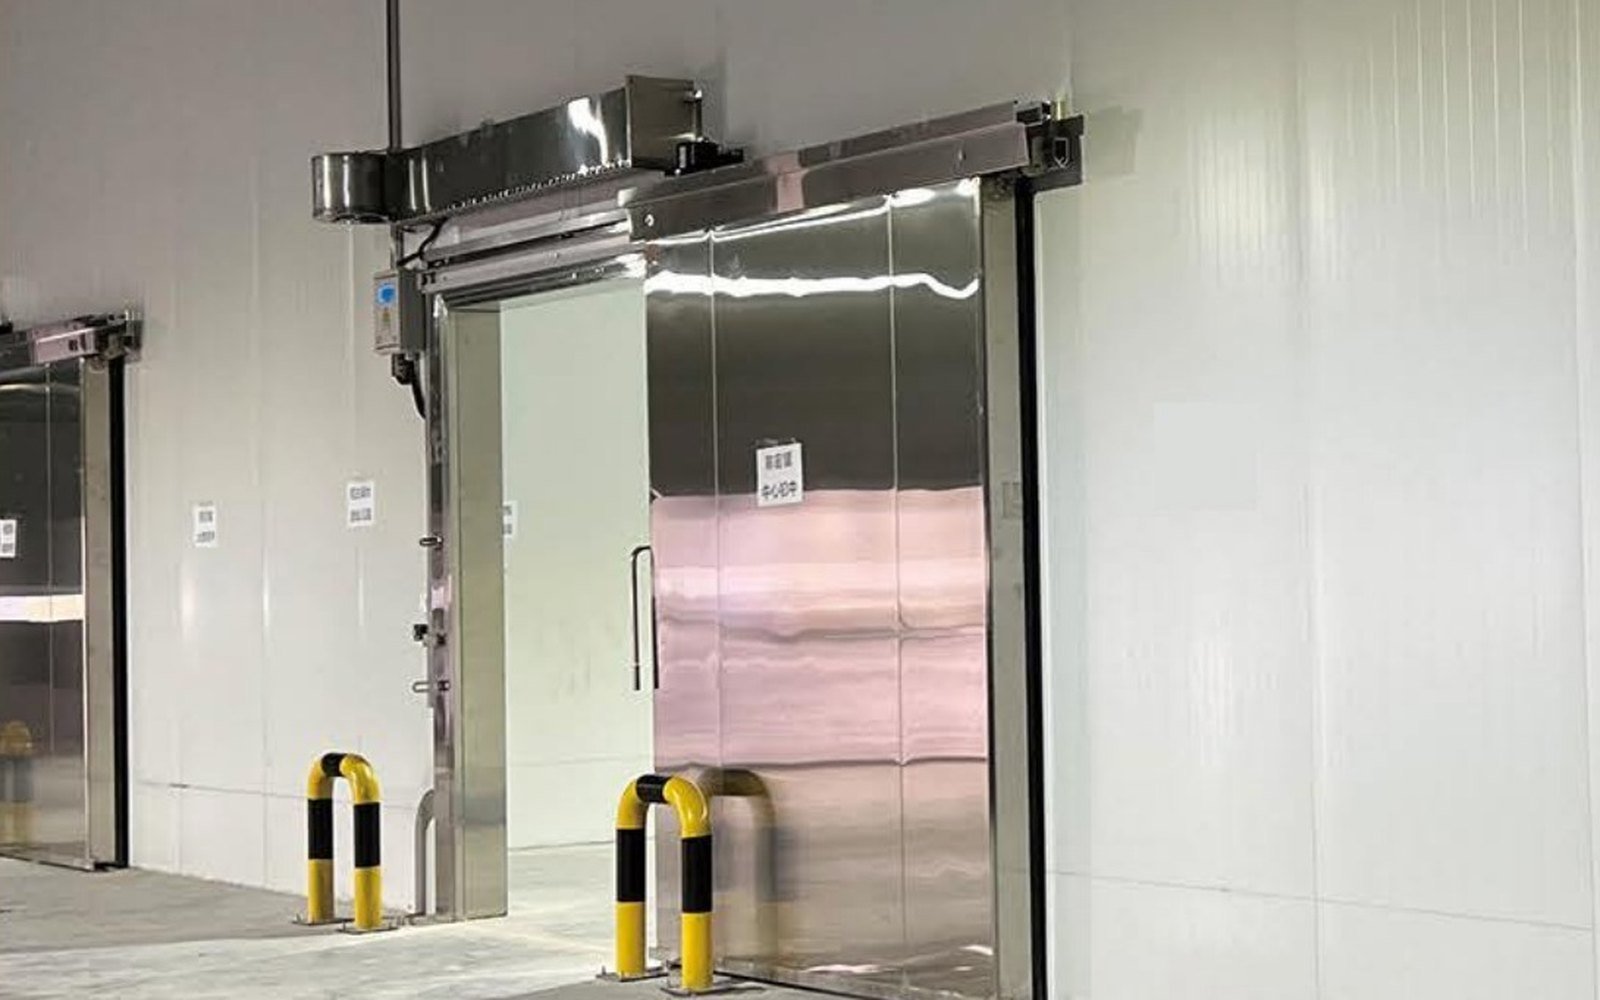
A distribution centre is a throughput problem, not a storage problem. The layout has to keep chilled, frozen and ambient flows separate while minimising door-open time at the loading dock. We design multi-temperature rooms, dock levellers, air-cushion and rapid-roll doors, and insulated dock shelters.
Industry
Pharmaceuticals
Validated temperature control and clean-room grade panels and doors.
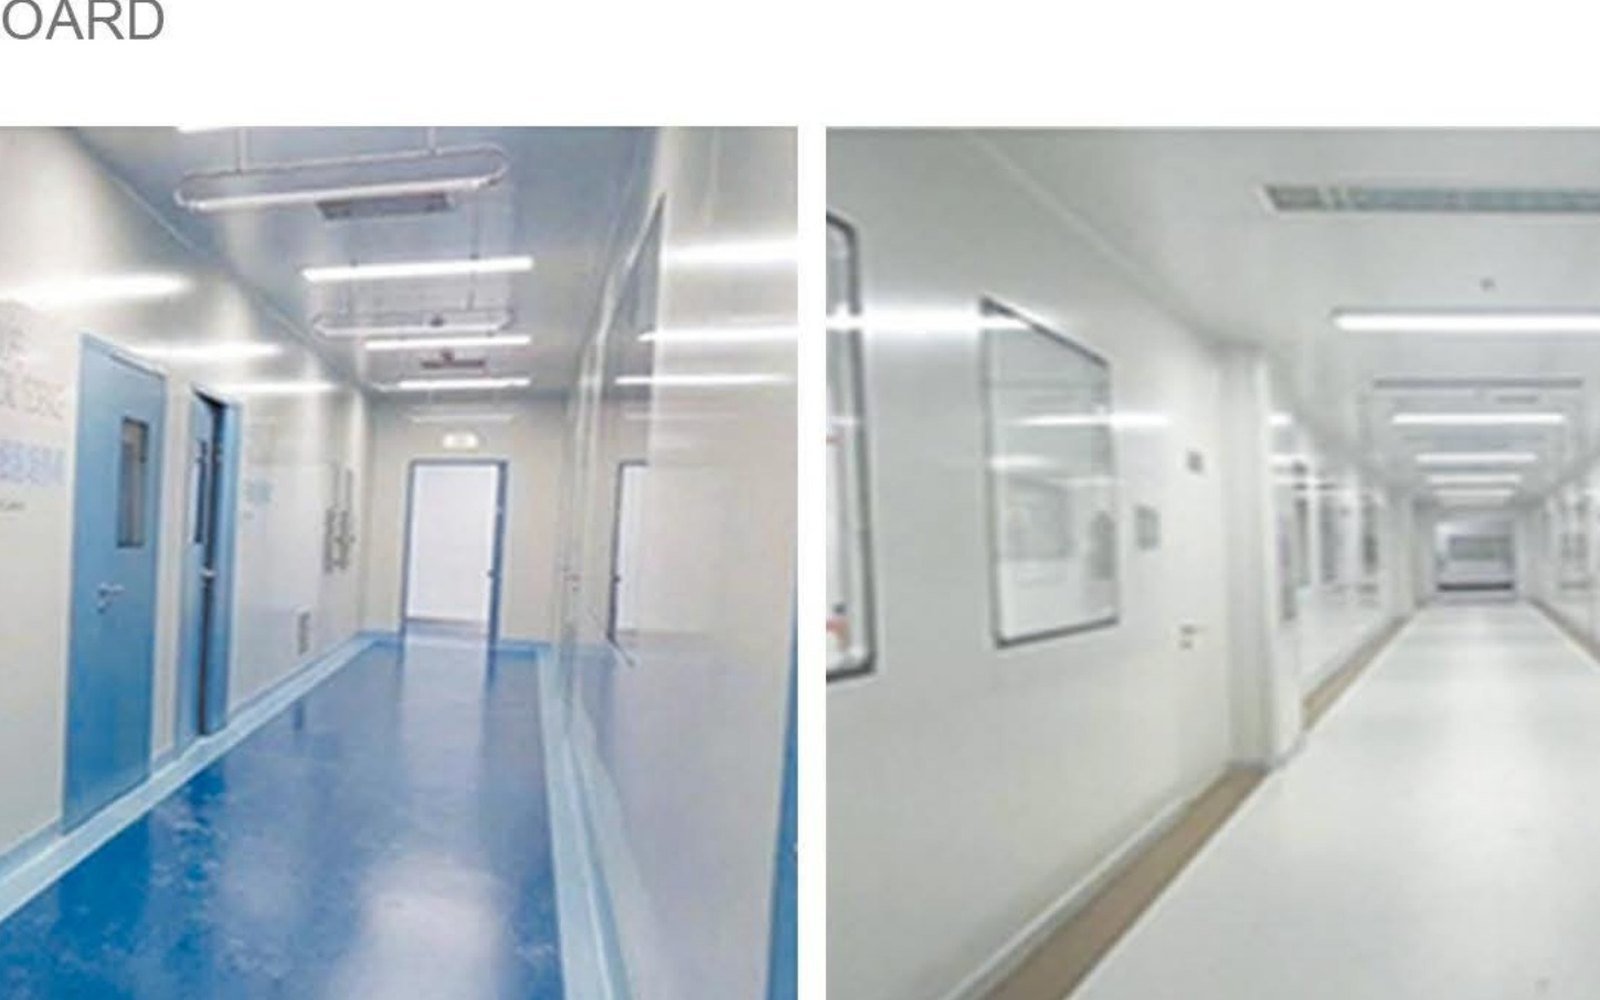
Pharmaceutical storage demands documented, repeatable temperature control and surfaces that can be cleaned and validated. We supply clean-room grade panels and doors, redundant refrigeration with automatic changeover, and monitoring points positioned for validation rather than convenience.
Send Us Your Plant. We’ll Send Back a Layout and a Price.
Tell us the product, the throughput and the room temperature. We’ll come back with an equipment selection, a layout drawing and a delivered price.